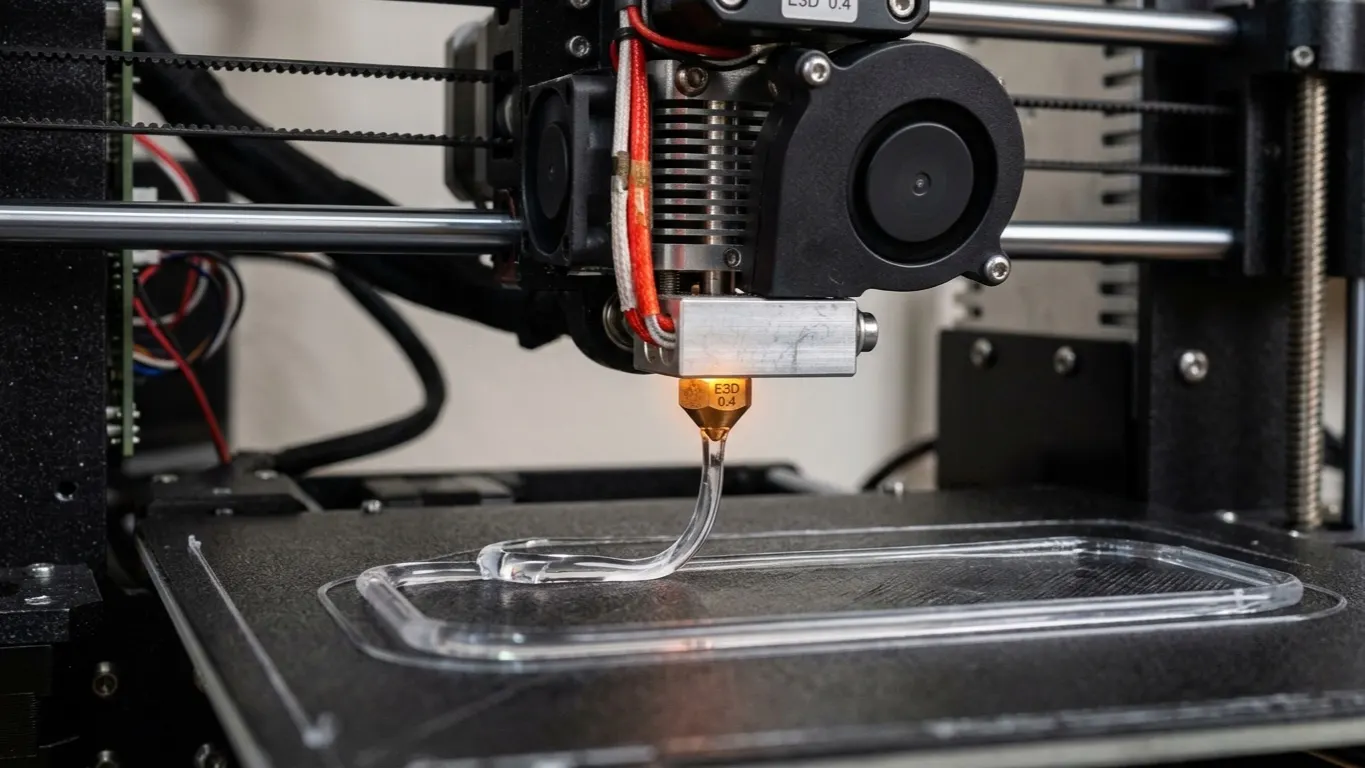
You set print speed to 300 mm/s in the slicer and nothing changes. It happens to everyone, and the reason is that your speed is not set by the number you type. It is set by how much plastic the hotend can melt per second, which is volumetric flow, measured in mm³/s.
Once you are against the flow limit, raising the speed setting does nothing; the printer is already at the end of what it can do.
The calculation
The plastic leaving the nozzle each second comes from three numbers:
flow (mm³/s) = layer height × line width × speed
0.2 mm layer, 0.42 mm line width, 150 mm/s:
0.2 × 0.42 × 150 = 12.6 mm³/s
Now compare that against what the hotend can actually deliver. Roughly:
| Hotend | Limit in Bambu's profile |
|---|---|
| Standard 0.4 mm, Bambu PLA Basic (X1C) | 21 mm³/s |
| High Flow 0.4 mm, Bambu PLA Basic (X1C) | 29 mm³/s |
| Standard 0.6 mm, Bambu PLA Basic (X1C) | 21 mm³/s, same as 0.4 mm (29 with High Flow) |
| Standard 0.4 mm, Bambu PETG Basic (X1C) | 15 mm³/s |
| Standard 0.4 mm, Bambu PETG HF (X1C) | 21 mm³/s, same as PLA Basic |
The 12.6 mm³/s above sits well under Bambu's standard-hotend figure, and even 200 mm/s, at 16.8 mm³/s, stays inside it. Push past the cap and the slicer throttles the flow; set the cap higher than the hotend can really melt and you get under-extrusion, gappy walls and weak layer bonding.
The filament has a limit too
The flow ceiling does not come from the hotend alone. The filament itself stops melting all the way through above a certain rate.
Some manufacturers give a maximum volumetric speed on the spool or datasheet. If yours does not, Orca Slicer's Max volumetric speed test measures it, and so does Max flowrate under More... in Bambu Studio's Calibration menu, which only shows up for a Bambu printer once Develop mode is on. Both print a wall at rising flow, and you look for where it breaks down. A change in flow can also show up as a change in sheen; see matte PLA printing shiny in spots.
Enter that value in the slicer and the printer will not exceed it, whatever your speed settings say; it throttles itself. That is the right way round: leave speed free and cap the flow. Why the Generic preset holds that cap at 12 mm³/s for non-Bambu filament is in Bambu PLA vs Generic PLA.
The number the test gives is the limit where extrusion breaks down; how far below that limit to stay on a load-bearing part is in volumetric speed and part strength.
How nozzle diameter changes speed
Going from 0.4 to 0.6 mm widens the line, so more plastic flows at the same speed. But the real gain is elsewhere: fewer lines, fewer layers.
With a 0.6 nozzle you can print 0.3 mm layers. The same part finishes in a third fewer layers at 0.3 than at 0.2. That alone cuts real time off the print, with the speed setting untouched.
The cost is detail. Fine text, sharp corners and small features disappear at 0.6. A good trade on a functional part, not on a miniature.
When walls are thin
A related problem: thin walls on the model do not print at all, or come out gappy. Speed is not the cause here. The wall is thinner than the nozzle's line width, so the slicer cannot fit a line in there and skips it.
In Bambu Studio and Orca the fix is under Quality:
| Setting | What it does |
|---|---|
| Wall generator: Arachne | Produces variable-width lines that adapt to thin areas |
| Minimum wall width | Default 85% of nozzle diameter: how wide the wall replacing a thin feature prints |
| Minimum feature size | Default 25%: thinner features are dropped, thicker ones are widened to Minimum wall width |
Classic keeps one line width and fills very thin spots with gap fill; Arachne varies the width as it goes. If a thin wall comes out gappy, this is the first setting to try.
A model that looks complete in Prepare but comes out with pieces missing in Preview has the same cause, and lowering the line width can also help there; the details are in the skipped thin parts article.
Practical order
- Find or measure your filament's maximum volumetric speed.
- Enter it in the slicer.
- Leave the speed settings alone; the flow cap will do the braking.
- Want it faster? Raise layer height, not the speed number.
- Still not enough? Go up in nozzle diameter.
Fiddling with the speed number comes last on the list, because that is where it makes the least difference. Where to change speed is covered separately.